IN Brief:
- Incada Duo extends Holmen’s existing Workington-produced paperboard range into laminated grades weighing 430–710 gsm.
- The company targets premium beverages, cosmetics, confectionery and gift cartons requiring greater thickness and print quality.
- Food-contact claims concern approved raw materials, while specific finished packs and unquantified environmental benefits require further assessment.
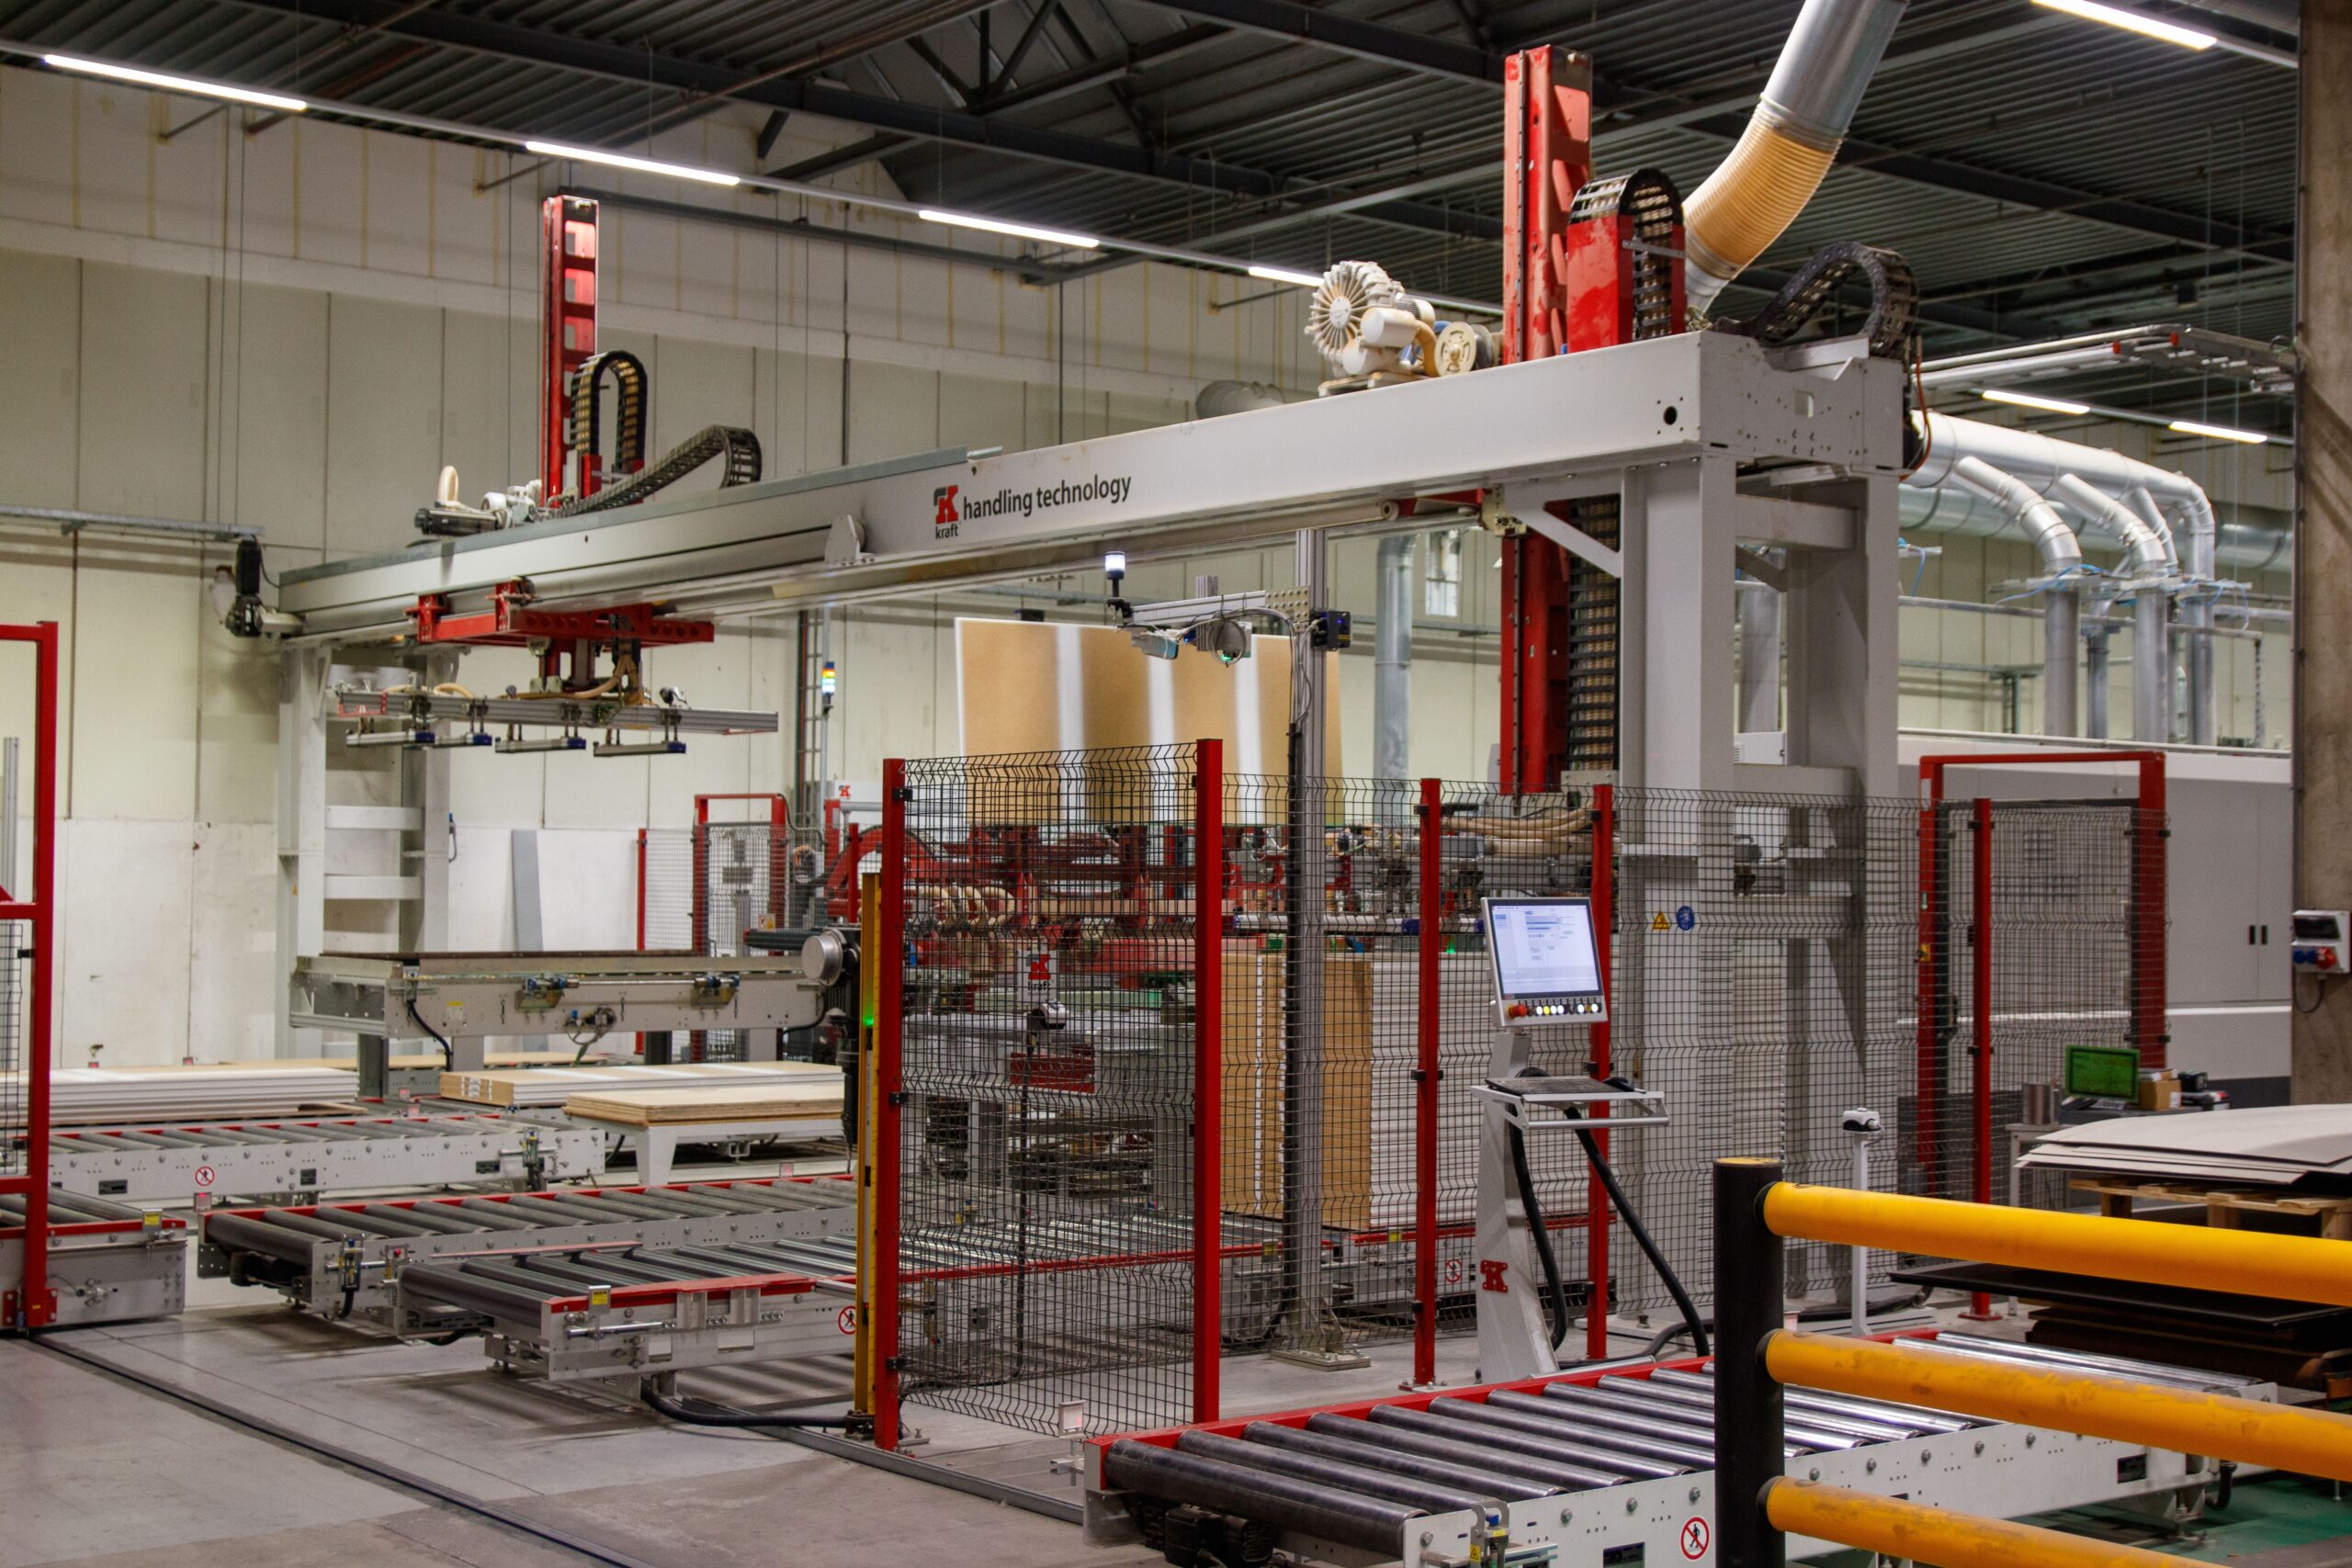
Holmen has introduced Incada Duo, a laminated folding box board produced in the UK for cartons requiring higher thickness and stiffness. The addition to its Incada paperboard range is offered at 430–710 grams per square metre (gsm) for applications including premium beverages, cosmetics, confectionery and gift packaging. The board originates from Holmen’s Workington manufacturing operation in Cumbria and is laminated within the UK, according to the company.
The established Incada family was launched in October 2001 and is associated with Holmen’s Workington mill in Cumbria. Incada Duo adds higher-caliper laminated construction rather than replacing that existing range. The company has not stated a dedicated production capacity, capital expenditure figure or confirmed customer order associated with the product launch. Its specification therefore establishes the grades being offered, not the number of tonnes that will be sold or converted during a particular period.
Grammage identifies the mass of one square metre of board; caliper measures sheet thickness. Lamination, fibre composition and coatings influence the relationship between those measurements, so the 430–710 gsm range cannot be translated into a universal thickness figure. Carton specifications must also account for bending stiffness, creasing behaviour, printed finish, weight and the load imposed by the contents. A higher grammage can provide more material for a demanding design, but it is not necessarily the lightest or lowest-cost solution for every pack.
Incada Duo combines multiple board layers to produce the higher-caliper construction, with fully coated outer surfaces based on white chemical sulphate pulp. Those surfaces are intended to support detailed graphics and finishing, while the laminated body supplies structural stiffness. Printers and converters will still need to test ink adhesion, die-cutting, scoring, folding and gluing with the chosen grade. Holmen has not provided independently verified strength comparisons or a universal performance advantage over named competing products.
Holmen says the raw materials used for Incada are approved for food contact and that the board is designed to avoid unwanted taint and odour. That statement does not certify every finished carton configuration. The suitability of inks, coatings, adhesives, barriers and any direct-contact surface depends on the food, its storage conditions and the applicable compliance documentation. Packaging used around sealed confectionery has different contact requirements from material directly touching an unpackaged product, even when both use the same base board.
Premium spirits, cosmetics and confectionery often require packaging with a substantial feel and well-defined visual appearance. Carton developers may use multiple panels, precision creases and decorated surfaces to achieve those properties without relying solely on secondary inserts. Incada Duo broadens the materials available for that design work, although Holmen has not identified particular brands adopting the new board. Whether a given format can switch from another substrate depends on trials using the actual carton geometry and converting equipment.
The new grade gives British converters a domestic paperboard manufacturing source at Workington, with lamination also undertaken in the UK. Holmen reports that the mill has run on fossil-free bioenergy since 2013. Domestic sourcing may shorten one part of a converter’s supply route compared with an imported alternative, but the actual freight saving depends on supplier and customer locations, ordered quantities and onward distribution. The product launch provides no measured reduction in delivery kilometres or a named customer’s supply chain emissions.
Holmen argues that the board’s stiffness and relatively low weight can support material-efficient carton designs. The environmental comparison, however, depends on the exact carton, competing substrate, processing losses and end-of-life route. No Incada Duo-specific carbon footprint, quantified transport saving or comparative life-cycle assessment accompanies the launch. Recyclability likewise has to be considered for the converted package, including any added laminates, coatings, windows or adhesives, rather than inferred solely from the fibre used in the base board.
Carton procurement involves more than the headline sheet specification. Buyers need to establish available sizes and grades, delivery lead times, print trials, quality tolerances and any documentation required for intended contact uses. A laminated grade may require different creasing rules or tooling settings from a single-layer material. Converters also need predictable supplies during repeated production runs so that print, folding and glue application behave consistently across batches.
Holmen has not identified a customer order, annual production volume or grade-by-grade rollout timetable for Incada Duo. Converters evaluating the 430–710 gsm range will need to qualify it against the dimensions, printed finish and folding performance of actual cartons before committing production runs. The confirmed step is a UK-made higher-caliper addition to a paperboard family first introduced in 2001, rather than a disclosed capacity expansion at the Workington mill.